
ISO 9001
ISO 14001
FDA
REACH
RoHS
CMA
CNAS
Core Advantages of StarColor Water-based Ink
Engineered for high-speed stability, global safety compliance, and superior print clarity.
Global Safety & Compliance
VOC-free and fully compliant with FDA, REACH,
and RoHS standards for food packaging.
High-Speed Stability
Optimized for gravure and flexo presses, maintaining consistent performance at speeds up to 400m/min.
Exceptional Adhesion & Rub Resistance
Superior bonding strength on challenging surfaces,
ensuring zero color fading after washing tests.
Versatile Substrate Compatibility
Engineered for non-woven fabrics, corrugated boards,
and various specialty paper products.
Technical Specifications of Water-Based Flexo Ink
The values below are the typical figures published in the technical manual and the SGS safety data sheet for this series, both downloadable below. Working viscosity and pH are fine-tuned to your press, substrate and drying system — the exact figures for your order are confirmed on the TDS that ships with the sample.
| Parameter | Typical value | Basis |
| Solid content | 30% – 40% | Technical manual |
| Working viscosity | 20 – 30 s at 25 °C | DIN 4 cup, technical manual |
| Product viscosity | 100 – 500 cps (dynamic) | SGS safety data sheet |
| pH value | 7.5 – 9.0 at 25 °C | Technical manual |
| Density | 1.0 – 1.2 g/cm³ | SGS safety data sheet |
| Gloss | 40% – 60% at 60° | Technical manual |
| Drying | Fully dry within 24 h; recommended oven 50 – 80 °C | Technical manual and white paper |
| Printing speed | 150 – 400 m/min | Technical manual |
| Anilox roller | 400 – 600 LPI for solid areas, 800 – 1000 LPI for fine graphics | White paper |
| Dilution | Deionised water, same-series diluent, or pH adjusting solution | Technical manual |
| Flash point | > 200 °C (non-flammable) | SGS safety data sheet |
| Shelf life | 12 months sealed, stored at 5 – 30 °C away from light | Technical manual |
Two numbers decide print quality on press. Viscosity: keep it within ±2 s of your target and re-test every 2 hours. pH: hold it between 8.0 and 9.0 and re-test every 4 hours — amine neutralisers evaporate as the ink circulates, and a drifting pH is the most common cause of a job that runs well for two hours and badly for the next six.


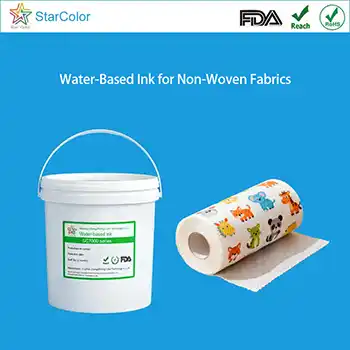
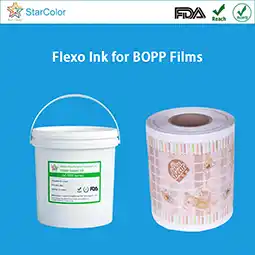

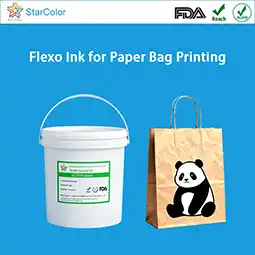

Substrate Compatibility
Optimized for non-woven fabrics, corrugated paper, and diverse flexible packaging.
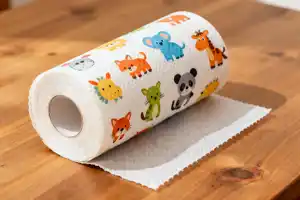
Nonwovens
Various non-woven products such as masks, shoe covers, table cushion covers, etc
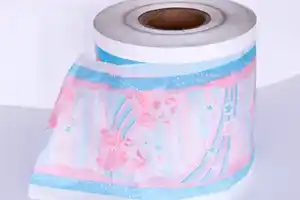
Plastic film
PP,BOPP,PET,LDPE,HDPE,Aluminum foil
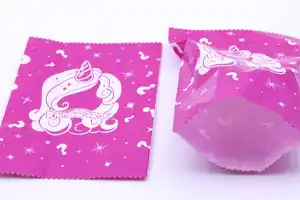
Paper and cardboard
copperplate paper,corrugated paper, cardboard, etc
Direct Food-Contact Compliance for Flexo Ink
"Food-safe ink" covers two very different requirements, and mixing them up is the most expensive mistake in food packaging. Decide which one applies before you choose a grade.
Direct food contact
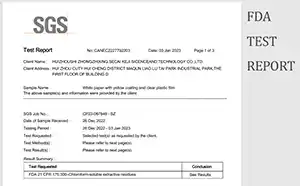
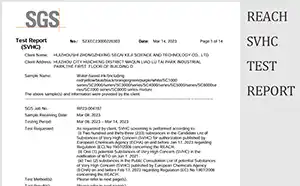
The print sits on the food-facing surface: paper cups, cake boards, napkins, straws, wrappers with no barrier layer. These jobs need a low-migration formulation built only from raw materials that stay inside the migration limits of the destination market. StarColor supplies FDA-tested flexo grades for direct contact — the FDA and REACH SVHC 236 reports are available for download on this page.
Indirect contact (reverse printing)
The print is buried behind a lamination or a coating, which is the usual structure for flexible packaging. The ink never touches the food, so what matters is low odour, no set-off during rewinding, and no migration through the adhesive layer. Our low-migration grades are built for exactly this case.
What we need from you
Tell us the substrate structure (film or paper, thickness, barrier layer), the food type and its fat content, the filling or retort conditions, and the destination market. We will recommend the matching grade and send the relevant test report and TDS before you commit to a trial run.
Quality Certifications & Test Reports
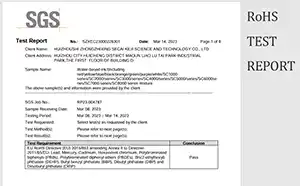
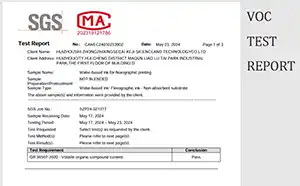
Fully compliant with FDA, REACH, and RoHS standards.
Flexo or Gravure? Choosing the Right Ink
Most packaging converters run both processes, and source ink for both. Here is how the two compare when you are deciding which ink to specify.
| Flexographic | Gravure | |
| Image carrier | Photopolymer plate with anilox roller | Engraved copper cylinder |
| Best for | Corrugated board, paper bags and cups, labels, non-wovens; short to medium runs | Flexible packaging film; long runs and fine detail |
| Water-based ink | Excellent on absorbent substrates | Well suited to paper and to treated film with the right drying |
| Ink range | This page — water-based flexo inks | Water-Based Gravure Ink |
StarColor manufactures the full set — water-based flexo, water-based gravure and UV / UV-LED inks — so a converter can qualify one supplier, one certificate pack and one country of origin for the whole press room. If you are still weighing up the two processes, start with these pages:
What is Water-based flexo ink?
Water-based flexo ink, a specialized liquid ink designed for flexographic (relief) printing, represents the future of sustainable packaging. Engineered for high-efficiency production, our formulas support press speeds exceeding 400 m/min, effectively eliminating traditional concerns regarding drying times.
As a 100% water-dilutable solution, it is completely free of organic solvents and VOCs. This odorless, eco-friendly chemistry not only ensures a safer workplace for operators but also aligns perfectly with stringent international environmental regulations.
Water-based flexo ink formula
| Serial | Name | content |
| 1 | water-based resin | 30% |
| 2 | pigment | 35% |
| 3 | Water | 34% |
| 4 | Other additives | 1% |
What each component does
| Component | Typical share | Function in the ink |
| Water-soluble resin (acrylic copolymer) | 30% | Forms the film and bonds it to the substrate; sets gloss, rub and water resistance |
| Organic pigment | 35% | Colour strength, opacity, and light and heat fastness |
| Deionised water | 34% | Carrier and diluent — replaces organic solvent, which is why VOC is essentially zero |
| Additives | 1% | Wetting agents, defoamers and levelling agents that control flow-out, foam and drying |
Resin and pigment together make up the solid fraction, 30 – 40% of the total weight. Where a job needs more gloss or better water resistance, the resin-to-pigment ratio is shifted towards 4:1 – 5:1 and a crosslinker is added before the run.
Common Flexo Ink Problems and How to Solve Them
Six of the issues converters report most often when running water-based flexo ink, with the fix recommended in our own white paper, which covers 24 problems in full.
1. The ink dries too slowly
Almost always the workshop, not the ink: humidity above 70% RH or a temperature under 20 °C, or a viscosity set too high. Raise the oven to 50 – 80 °C and dilute with deionised water to 25 – 35 s at 25 °C on a No. 4 cup.
2. Poor adhesion on film
Surface energy, not the ink. Corona-treat the film to at least 38 mN/m before printing; if the structure still will not hold, add 3 – 5% polyurethane adhesion promoter.
3. pH drifts during a long run
Amine neutralisers evaporate as the ink circulates. Test pH every 4 hours and top up with ammonia water or an amine stabiliser, no more than 1% per addition, and keep the circulation system sealed.
4. Foaming in the ink pan
Shear at high press speed, or too little defoamer. Add 0.1 – 0.5% pre-dispersed silicone defoamer and reduce pump speed.
5. Anilox cells clogging or plate filling in
Skinning inside the cells, contamination, or incomplete cleaning. Filter the ink through 5 – 10 µm before loading, add 1 – 3% slow-drying agent, and clean the anilox rollers daily with a pH-neutral cleaner.
6. Weak rub and scuff resistance
The dried film is not hard enough. Select a high-Tg acrylic-polyurethane resin, add 2 – 4% nano-silica, or overprint with a water-based varnish at 1 – 2 µm dry film thickness.
Download the full guide: Flexographic Water-based Ink Use White Paper (PDF, 24 problems). If a job is still misbehaving, send us the substrate, the ink code and your press settings and our engineers will work through it with you.
Essential FAQ for Flexo Ink Solutions
Q1: What are the primary advantages of using water-based flexo ink for packaging?
A: Water-based flexo ink is highly preferred for its eco-friendly profile, featuring low VOC emissions and a non-flammable nature. It provides excellent color density and stability on absorbent substrates like paper and corrugated board, making it the safest choice for food-grade and medical packaging.
Q2: Can your flexographic inks achieve high-speed printing on plastic films?
A: Yes. While water-based inks are traditionally used for paper, our advanced flexographic ink formulations are engineered with superior adhesion and fast-drying properties for treated PE, PP, and BOPP films. They support stable, high-quality output at press speeds exceeding 400 meters per minute.
Q3: How do you ensure the color consistency of flexo inks across different batches?
A: As a professional flexo ink manufacturer, we utilize automated color management systems and rigorous QC testing. Each batch is verified against Pantone standards and customer-approved master samples to ensure precise color reproduction and minimal Delta E variance.
Q4: Are your flexo ink products compliant with FDA and REACH regulations?
A: Absolutely. All our flexo printing inks are formulated to meet international safety standards. We provide fully compliant solutions that have passed FDA 21 CFR 175.300, EU REACH, and RoHS certifications, ensuring they are safe for food packaging and sanitary materials.
Q5: What technical support does StarColor provide for flexo ink troubleshooting?
A: We offer comprehensive technical assistance, including ink viscosity adjustment, pH value control guidance, and substrate compatibility testing. Our engineers can also help optimize your anilox roller selection and drying system settings to ensure peak printing performance.
Q6: What are the technical specifications of your water-based flexo ink?
A: Solid content is 30–40%, working viscosity 20–30 seconds at 25°C on a DIN 4 cup, pH 7.5–9.0, density 1.0–1.2 g/cm³ and gloss 40–60% at 60°. The ink runs at 150–400 m/min and is fully dry within 24 hours. Exact figures for your order are confirmed on the TDS shipped with the sample.
Q7: Do you supply inks for direct food contact?
A: Yes. We supply FDA-tested low-migration grades for print that touches the food directly, such as paper cups, cake boards and napkins, as well as low-migration grades for reverse-printed laminates where the ink sits behind a barrier layer. Send us the substrate structure, food type and destination market and we will recommend the matching grade.
Q8: Can I source both flexographic and gravure ink from StarColor?
A: Yes. We manufacture water-based flexo ink, water-based gravure ink and UV / UV-LED ink, so a converter running both processes can qualify a single supplier, one certificate pack and one country of origin for the whole press room.
Contact Us
Our engineers are ready to help you optimize your ink viscosity, pH control, and adhesion for high-speed flexo presses. Tell us about your substrate, and we'll provide a tailored quote within 24 hours.


Phone/WhatsApp
+86 18011968332


Address
Huidong County, Huizhou City, Guangdong Province,China